Information Details
Production process of American standard EN1092-1 P245GH flange
Release time:
2020-07-20
Source:
Production Technology of American Standard EN1092-1 P245GH Flange
1.American standard EN1092-1 P245GH flangeThe forging process generally includes the following steps, that is, selecting high-quality blanks for blanking, heating, forming and cooling after forging. Forging techniques include free forging, die forging and die forging. In the production process, different forging methods should be selected according to the quality of forgings and production batches.
2. Free forging has low productivity and large machining allowance, but its tools are simple and universal, soAmerican standard EN1092-1 P245GH flangeIt is widely used for forging simple single pieces and small batch forgings. Free forging equipment includes air hammer, steam air hammer and hydraulic press, which are suitable for the production of small, medium and large forgings respectively. Die forging has high productivity, simple operation, and easy realization of mechanization and automation. Die forgings have high dimensional accuracy, small machining allowance, and more reasonable fiber structure distribution, which can further improve the service life of parts.
3. Regardless of whether the annealing temperature reaches the specified temperature, the US standard EN1092-1 P245GH flange treatment generally adopts solution heat treatment, commonly known as "annealing", and the temperature range is 1040~1120. You can also observe through the observation hole of the annealing furnace that the flanged pipe fittings in the annealing zone should be incandescent, but there is no softening and sagging.
4.American standard EN1092-1 P245GH flangeThe water vapor is treated in a casting furnace. On the one hand, check whether the furnace body material is dry. When the furnace is installed for the first time, the furnace body material must be dry; second, whether there are too many water stains left in the flange pipe fittings entering the furnace, especially if there are holes in the flange pipe fittings, do not leak in, otherwise the atmosphere of the furnace will be completely destroyed.
5. The sealing of the furnace body, the American standard EN1092-1 P245GH flange bright annealing furnace should be closed and isolated from the outside air; when hydrogen is used as a protective gas, only one exhaust port is opened (for igniting the discharged hydrogen). The inspection method can be applied to the joints of the annealing furnace with soapy water to see if it is running; the place where the gas easily escapes is where the annealing furnace enters and leaves the pipeline. The sealing ring in this place is particularly easy to wear, so it should be checked and replaced frequently.
6. Protective gas pressure. In order to preventAmerican standard EN1092-1 P245GH flange, Slight leakage, the protective gas in the furnace should maintain a certain positive pressure. If it is a hydrogen protective gas, it is generally required to be above 20 kbar.
7. Annealing atmosphere: High-neck flanges generally use pure hydrogen as the annealing atmosphere, and the atmosphere purity is above 99.99%. If another part of the atmosphere is an inert gas, the purity may be lower, but it cannot contain too much oxygen and water vapor.
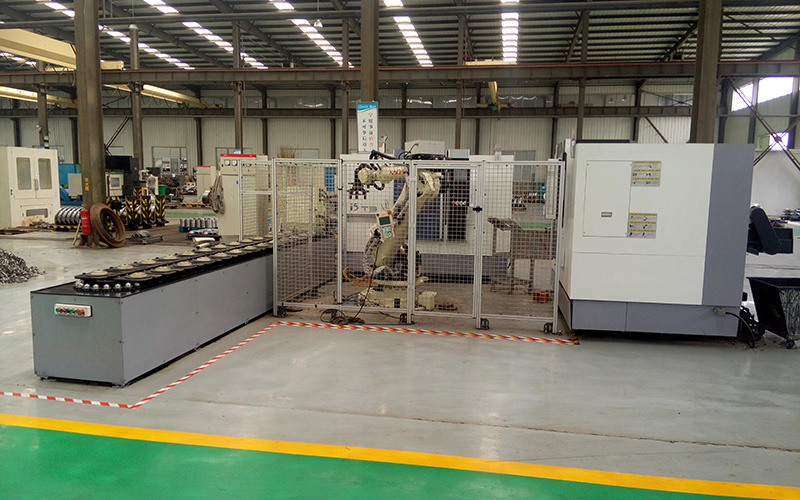
8. High-precision CNC lathe turning, CNC rocker arm drilling, and finally the American standard EN1092-1 P245GH flange forming.
American standard EN1092-1P245GH flange, marine DNV,LR Flange, Carbon Steel Stainless Steel Body Forging, A105 Blind BL Flange
SHANXI HAOKUN FLANGES GROUP CO.,LTD
Address: Fanglan Industrial Park, Dingxiang County, Xinzhou City, Shanxi Province
Fax: +86-350-6090 815
Zip Code: 035400
Large grinding ring 3 meters forgings mixer raceway carbon steel stainless steel valve body forgings

Copyright©2024 SHANXI HAOKUN FLANGES GROUP CO.,LTD
A105 blind plate BL flange-FPSO flange-alloy steel F11 high neck LWN flange-slewing bearing-large grinding ring 3 m forging-mixer truck raceway-rotating A694F52 A350LF2
A182F51 flange-oil casing-carbon steel stainless steel valve body forgings-American standard EN1092-1 P245GH flange-marine DNV LR flange